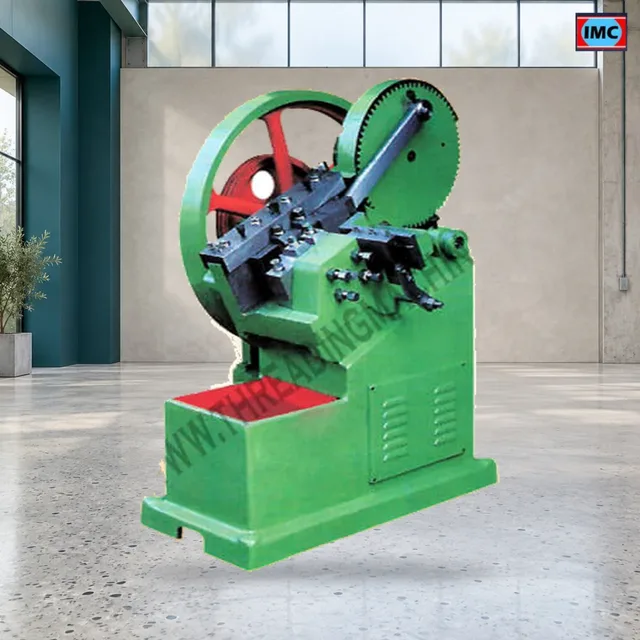
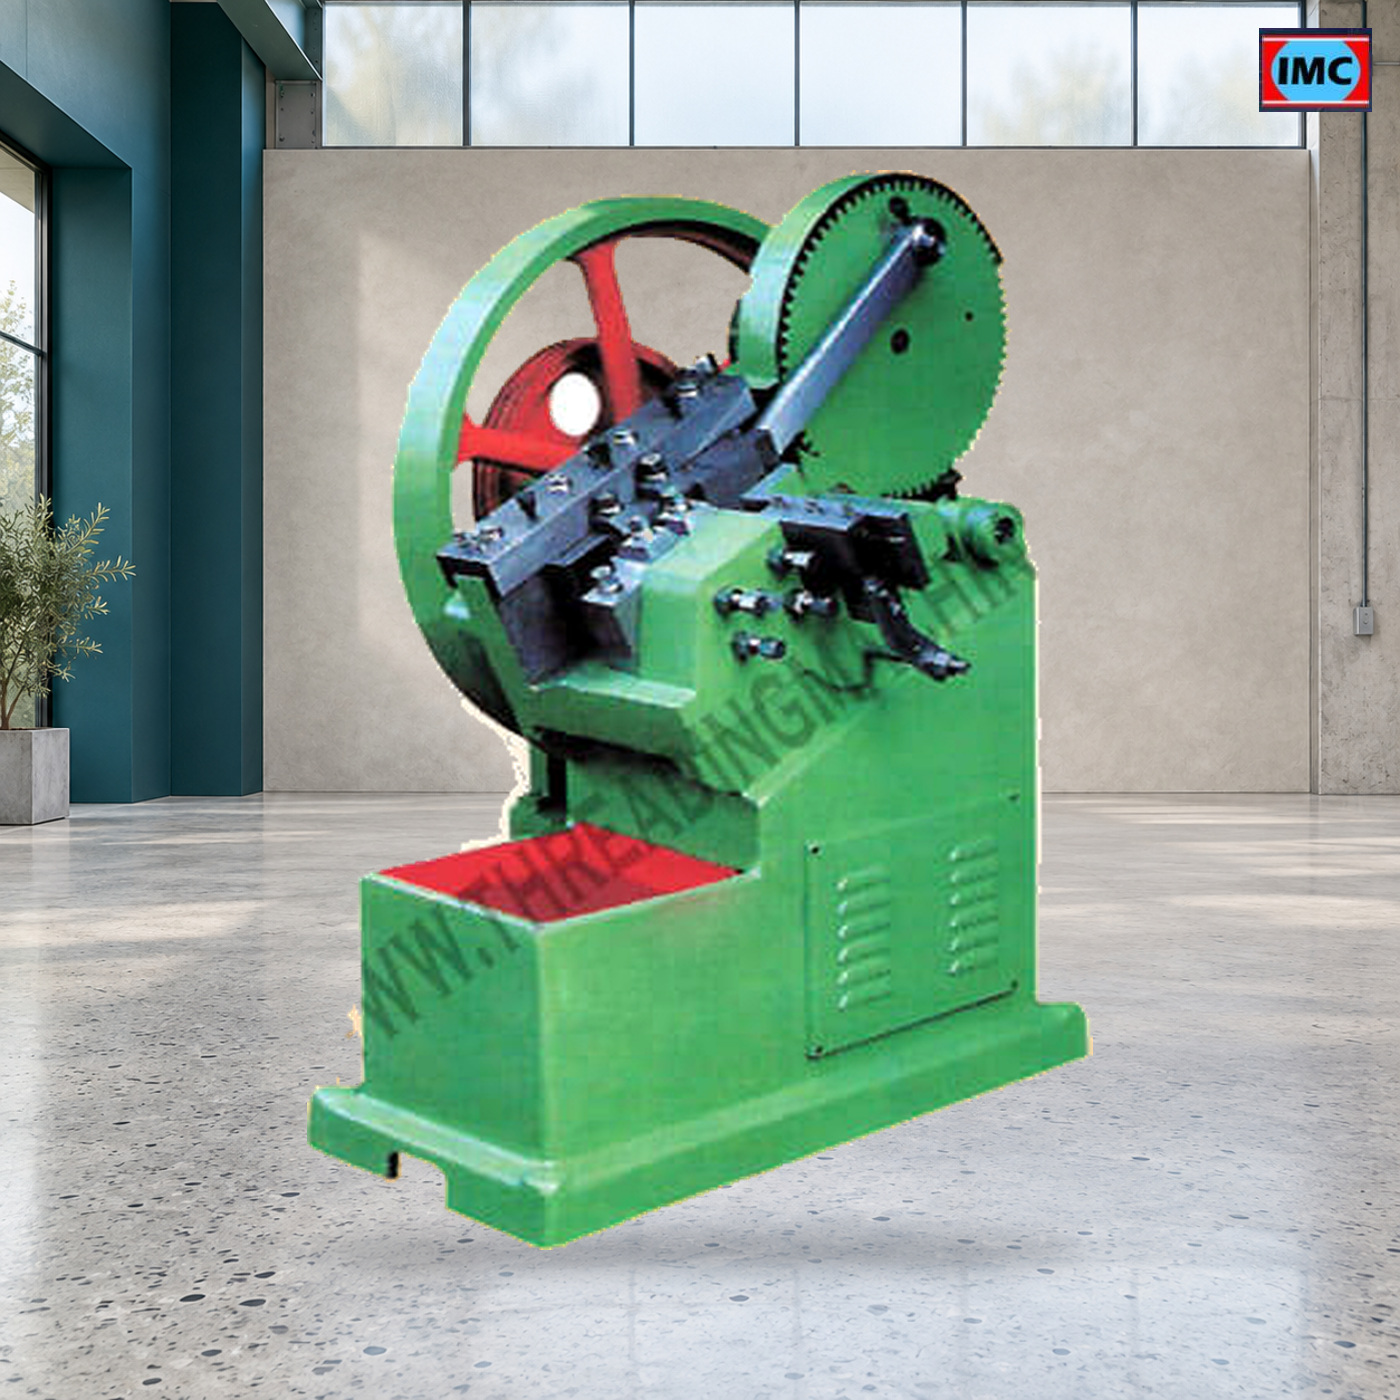
This guide explains the working process and selection of Flat Die Thread Rolling Machine.
Understand the working process
The purpose of this configuration is to form external threads on suitable fastener blanks between matched flat dies. The blank rolls between the matched flat die faces as their relative movement forms the external thread by material displacement. The process begins with a suitable component or starting stock and a defined result. Before selecting equipment, identify blank diameter and material, fastener shape, thread form and thread length. These requirements establish the operation to be performed and the information needed for the setup.
Review the setup sequence
The tooling and holding discussion includes flat-die geometry, blank presentation, feeding and changeover requirements. Check compatibility and the supplied operating guidance before starting a new job or changing a component size. The blank and flat-die profile should be considered together; this is cold forming rather than thread cutting. Preparation and any following production stage must be considered separately where the finished component needs additional work.
Check the result and select the model
The component review should cover formed thread dimensions, gauge acceptance and the condition of the blank. Agree the inspection requirements for a representative sample before comparing output estimates. Consult the specifications below and discuss the drawing and material with IMC. Select the available options and use the Quote List to request a configuration with clearly identified tools and accessories. This working overview supports selection; follow the instructions supplied for the actual machine.